APPLICATIONS
Pumping of Liquids and Slurries
Smart Pump Solutions with AI for Demanding Industries
The transfer of liquids and slurries is a critical process step in mining, power generation, municipal and industrial wastewater treatment, and many other industries. High and potentially fluctuating solids content, abrasive or chemically aggressive substances, and long delivery distances require reliable and robust pump systems.
For decades, ABEL has been a specialist in diaphragm and piston diaphragm pumps, offering customized solutions for the safe and economical transport of even the most challenging liquids and slurries. An innovation in our pumps is that they are equipped with intelligent pump monitoring with AI, which reduces operating costs and makes operation virtually worry-free.
Pumps suitable for this application
Recommendation:
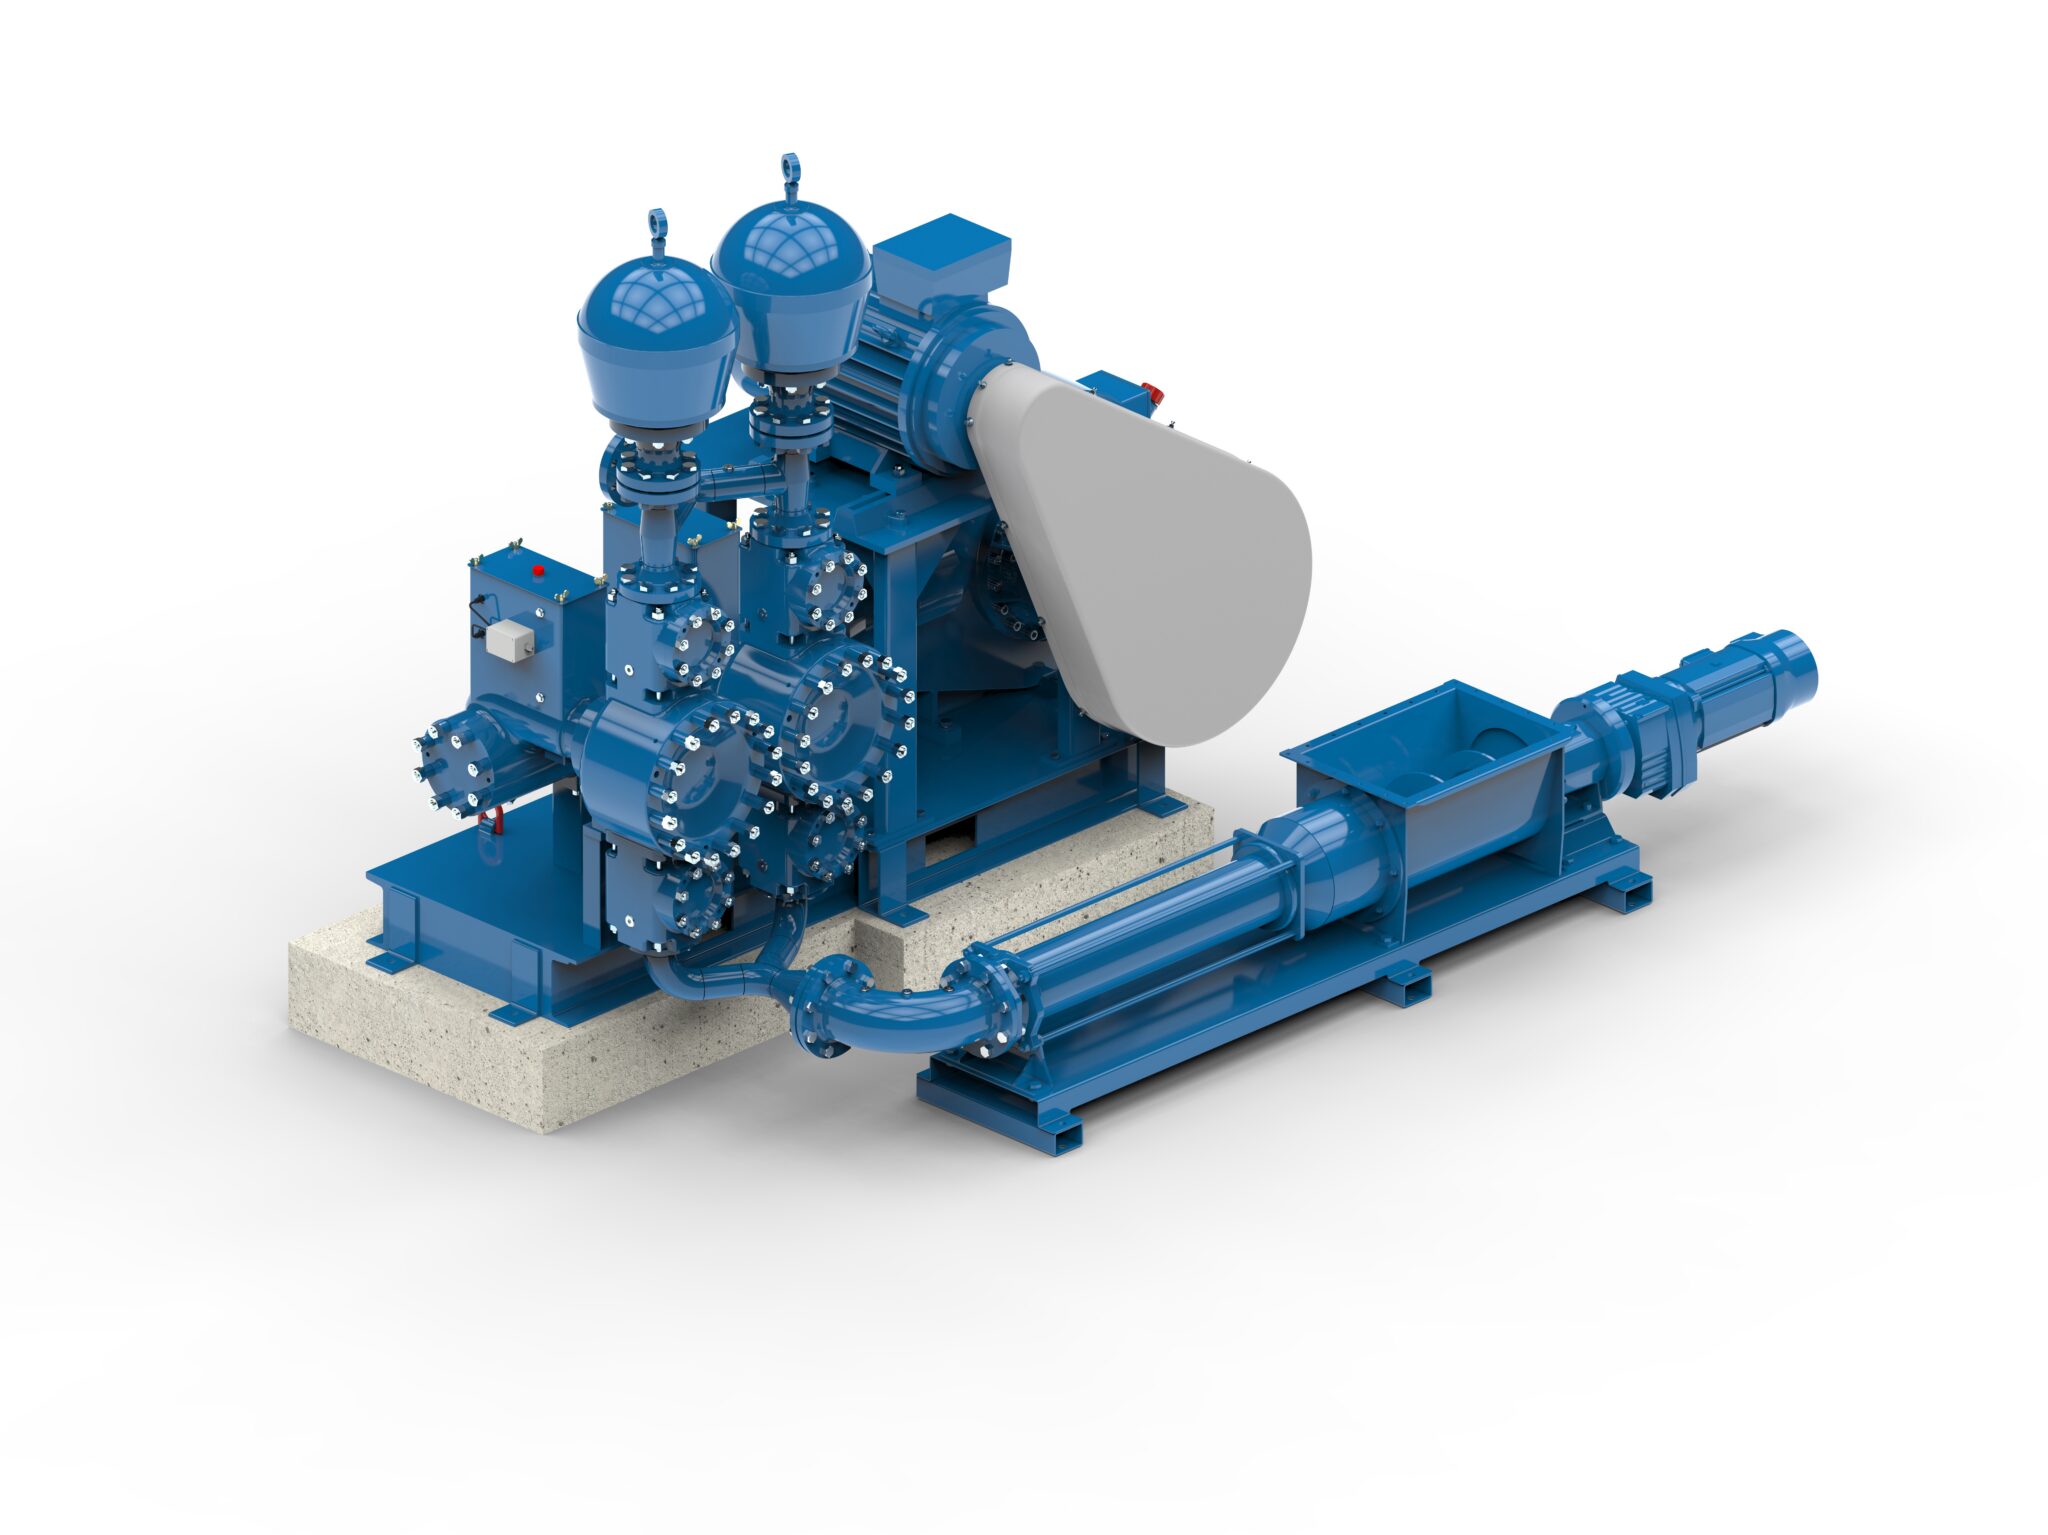
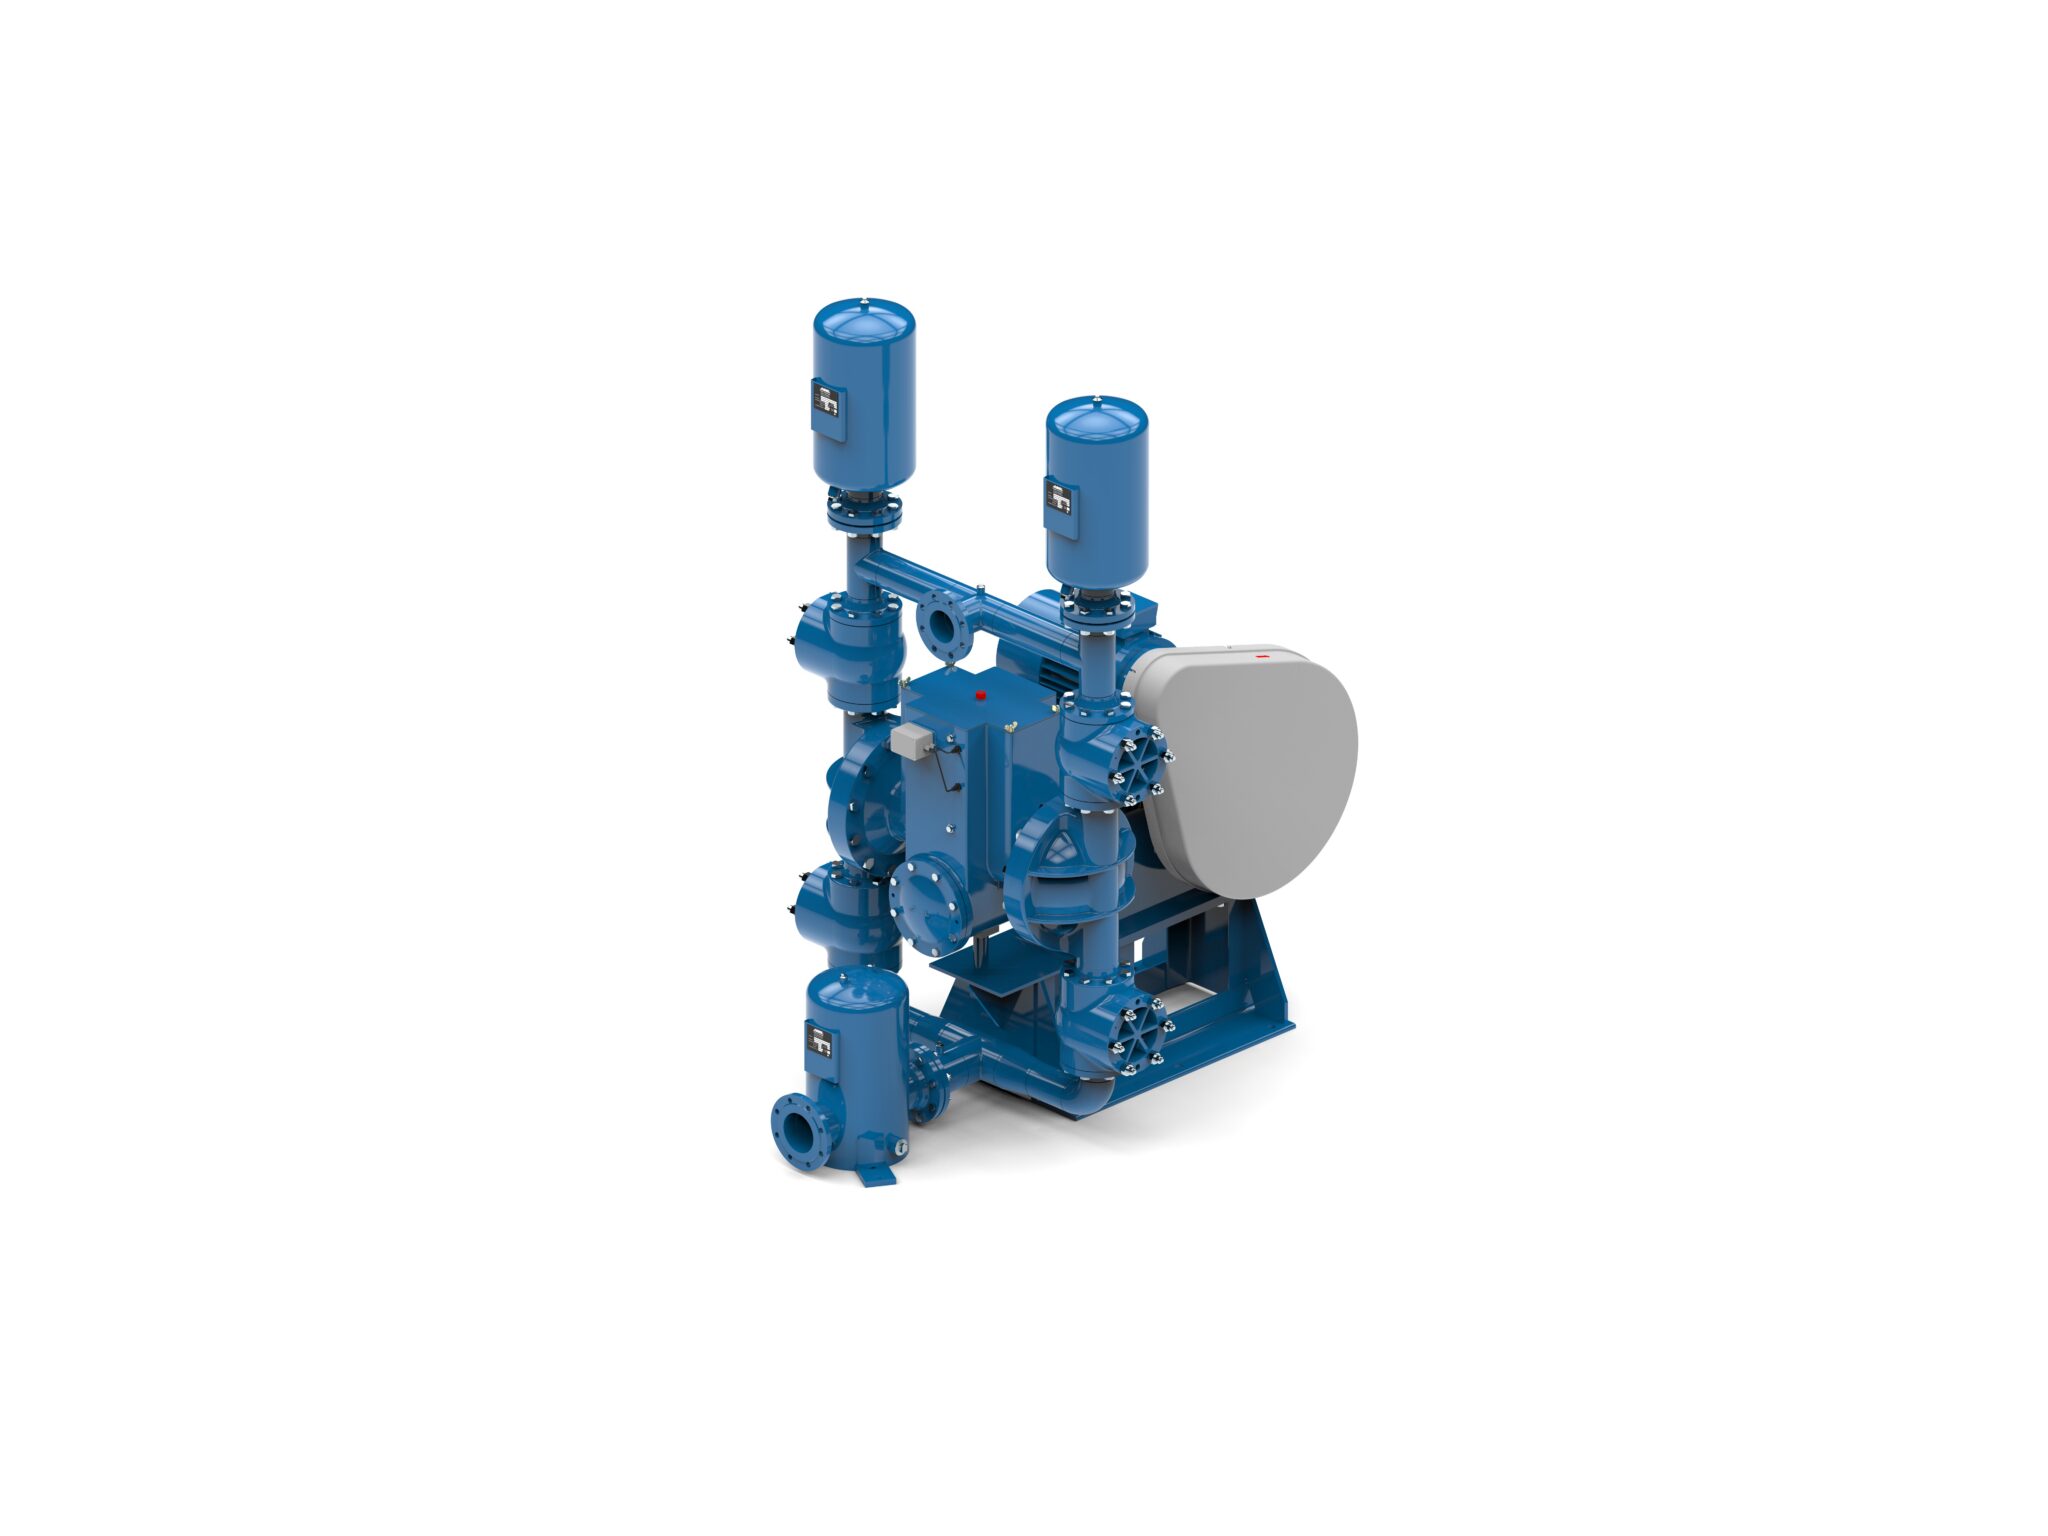
HMQ version of the HM series
Why ABEL Pumps?
- Specialist in manufacturing and development of positive displacement pumps
- Decades of experience in industry, mining, and environmental technology
- ABEL pumps ensure high system availability and process reliability
- Energy-efficient and durable solutions
- Intelligent AI pump monitoring
We offer pumping solutions for the transport of liquids, slurries, or slurries with a high solids content or dewatered slurries, tailored precisely to your process requirements.
ABEL – Your Partner for Safe and Cost-Effective Pump Systems
Liquids and Slurries Handled by our Pumps
ABEL pumps are used worldwide for a wide range of products, including:
Wastewater (municipal and industrial)
Raw, fresh, and secondary sludge (biological)
Sewage sludge and dewatered sewage sludge
Mining slurries/tailings
Fly ash and bottom ash
Foundry and steel mill slurries
Lime milk and lime slurry
Metal hydroxide slurries
Industrial sludge and filter cake
Grinding slurry
Oil sludge, oils, and fuels
Solvents and chemical liquids
Saltwater and salt solutions
Paints, varnishes, adhesives, and glues
Ceramic slip and slurries
and many more…
These media vary greatly in terms of viscosity, solids content, abrasiveness, and chemical composition. However, our wide range of pumps offers the right pump for every medium.
Transport of Wastewater
Municipal raw wastewater is untreated wastewater with a comparatively low solids content (approx. 1 %), but may contain sand, fibers, and hair. The use of piston diaphragm pumps is particularly beneficial when overcoming large height differences, long pipelines, and fluctuating flow rates. Conventional centrifugal pumps often reach their limits in these situations.
ABEL piston diaphragm pumps offer decisive advantages here:
- Resistant to clogging due to fibrous material
- Effortless handling of sand content (e.g., during heavy rain)
- High discharge pressures even over long distances
- Frequency-controlled operation to adapt to fluctuating wastewater volumes
This makes them ideal for demanding wastewater applications in municipal and industrial facilities.
Pumping Mining Tailings and Paste-Like Products
Open-pit and underground mining generate enormous volumes of tailings and ore slurries – often with solids content of up to 75 %. Transporting these over several kilometers requires extremely robust and fail-safe pump technology: the ABEL HMQ piston diaphragm pump.
Advantages of the HMQ in Tailings Transport:
- AI-powered pump monitoring for maximum pump availability
- Handling of very high solids concentrations up to 75 %
- Suitable for long conveying distances
- High energy efficiency
- Exceptionally long service life
In combination with AI-powered pump monitoring, system availability is maximized. The system continuously monitors the pump’s condition, detects deviations early on, and enables predictive maintenance, which minimizes unplanned downtime.
Fly Ash Transport in Power Plants
The operation of coal-fired power plants generates large quantities of fly ash. In the HCSD system (High Concentration Slurry Disposal), the ash is mixed with water to form a highly concentrated slurry and conveyed over distances of several kilometers.
Advantages of the ABEL HMQ Piston Diaphragm Pump for Fly Ash Transport
- AI pump monitoring for maximum pump efficiency
- Handling of solids concentrations up to 65 %
- The higher solids content means a significantly lower water content in the slurry compared to the use of centrifugal pumps
- Prevention of sedimentation through optional check valves
- Very long maintenance intervals
- Low total cost of ownership
The combination of the ABEL HMQ pump and AI pump monitoring ensures safe, efficient, and low-maintenance ash disposal.
Pumping of Dewatered Sewage Sludge
Dewatered sewage sludge poses particular challenges due to its high solids content. The ABEL SDS solids diaphragm solution enables:
- Early error detection through integrated AI monitoring
- Pumping of dewatered sewage sludge and pastes with up to 75 % solids content
- Easy maintenance (no complex hydraulics)
- Up to 80 % lower operating costs compared to hydraulic piston pumps
The combination of the ABEL SDS solids diaphragm solution and AI pump monitoring ensures safe, efficient, and low-maintenance conveying of dewatered sewage sludge.